
Introduction
I remember walking onto a shop floor and seeing three different turret lathes humming at once — the sound sticks with you. In many shops today, turret lathe manufacturers are judged by lead times and repeatable tolerance data (we tracked a 22% difference across suppliers last year). So how do you pick a partner that won’t slow you down or eat your margin? I’ll walk you through what actually matters — no jargon heavy fog, just what I’ve learned working with spindle setups, tool turrets, and CNC controls. Stick with me — we’ll get practical and clear as we move on.
Why the Old Fixes Fail: Hidden Faults in the Vertical Turret Lathe Machine World
I want to look under the hood of a vertical turret lathe machine and point out where the usual fixes miss the mark. Old approaches focus on shiny specs: bigger spindles, tighter advertised tolerances, or faster feed rates. But those numbers hide real pain — inconsistent indexing, slow tool change choreography, and poor control tuning that only shows up after a week of mixed runs. Look, it’s simpler than you think: a machine can read well on paper but wobble when the workpiece temp changes. Tool turret chatter, boring bar deflection, and marginal spindle bearings are the sneaky culprits. — funny how that works, right?
So what breaks first?
The short answer: the parts of the system that get ignored. Shops often skip thorough testing of dynamic stiffness, tool-path interpolation, and controller latency. Those omissions turn into scrap or rework later. I’ve seen shops try quick fixes — softer cutting parameters, bigger margins — but those bring cost, not answers. We need to be honest about where the traditional solutions fall short: they treat symptoms, not the system (indexing accuracy, torque control, and thermal drift are system-level problems).
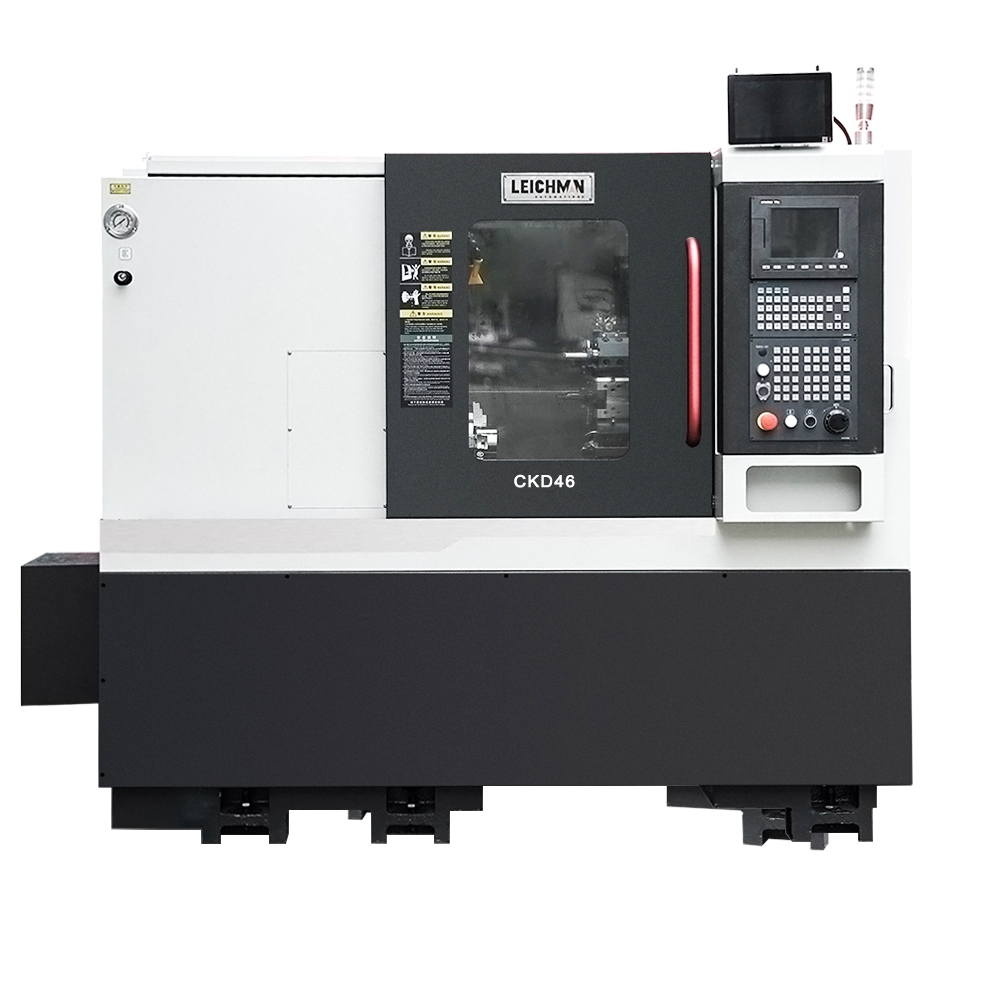
Looking Ahead: New Principles for Choosing CNC Vertical Turret Lathe Manufacturers
Let’s switch gears toward the future. When I evaluate potential partners now, I favor principles over promises. For example: modular drive systems that let you tune torque, closed-loop feedback on the turret index, and predictive maintenance hooks built into the controller. These are not buzzwords. They cut downtime and make setups stay true across shifts. If you’re scanning suppliers, you’ll want to ask about controller APIs, sensor integration, and spindle balancing routines.
What’s Next: Practical checks to use
Here are three quick checks I use to separate talk from real capability: 1) Run a mixed-material batch and measure first-pass yield; 2) Ask for a live demo of tool change timing under load; 3) Verify remote diagnostics and spare-part lead times. Those tests show whether a vendor is ready for real shop chaos. Also — test the vendor’s calibration story. If they can’t show regular, logged axis calibration, walk away. That’s a red flag.
Evaluation Metrics and Final Thoughts
To close, let me give you three clear metrics to weigh when choosing among cnc vertical turret lathe manufacturers: 1) First-pass yield under mixed runs (how many parts pass without adjustment); 2) Mean time to recover (how fast a machine is back online after a fault); 3) Real spare-part lead time plus remote diagnostic access. Use these numbers. They’re simple, measurable, and they map to real cost. I’ve used them to cut rework by double digits — not just on paper. — you’ll thank me later.
I want to be clear: I’m not selling a fairy tale. Picking the right partner takes hands-on checks and some blunt questions. But the payoff is real: fewer surprises, cleaner runs, and teams that sleep better. For a reliable source you can check, look up Leichman at Leichman.