
Introduction: a shop-floor moment, a stat, a question
I remember standing next to a tired machine on a Monday morning — chips everywhere, the operator rubbing his temples — and thinking, “We can do better.” Many of us in local shops nod when we talk about downtime; vertical machining center manufacturers are hearing that same groan from clients across the province. Recent shop-floor surveys show average machine availability closer to 70–80% (not the 95% managers promise), so I ask: why are so many centres still leaving capacity on the table?
That gap — between expected output and real output — matters. It eats profit. It frustrates teams. It slows delivery. So let’s dig in, yes? I’ll walk you through what I see every week, some hard numbers, and then a practical path forward — no fluff, just what works.
Part 2 — Where the old fixes fail: a technical look
When shops call a cnc vertical machining center supplier, they often expect a plug-and-play miracle. I’ve been on both sides of that phone, and honestly, many legacy fixes are cosmetic. They mask deeper issues. A quick retrofit might address spindle chatter for a month, but the root cause — bad tooling strategy or worn servo drives — stays. Look, it’s simpler than you think: spend time diagnosing, not just patching.
What’s really breaking down?
First, tooling routines are treated like folklore rather than data. Shops keep cutting speeds and feeds from memory, which leads to inconsistent surface finish and tool life. Second, control and integration problems pop up: older PLC logic or poor CAM software handoffs create nasty mismatches between program and machine. Third, the mechanical wear is often underestimated — bearings loosen, the tool changer misaligns, and spindle balance drifts. Those are industry truths: spindle speed matters, tool changer precision matters, and servo drives must be tuned. I mean it — you can tweak coolant pressure all day, but if the axis backlash is the issue, nothing changes.
So what do I recommend? Stop buying band-aids. Test toolpaths, log spindle rpm and torque, and review parts of the power chain like power converters and spindle bearings. I’ll say it plainly: short-term fixes cost long-term headaches. — funny how that works, right?
Part 3 — Looking ahead: practical future outlook and comparisons
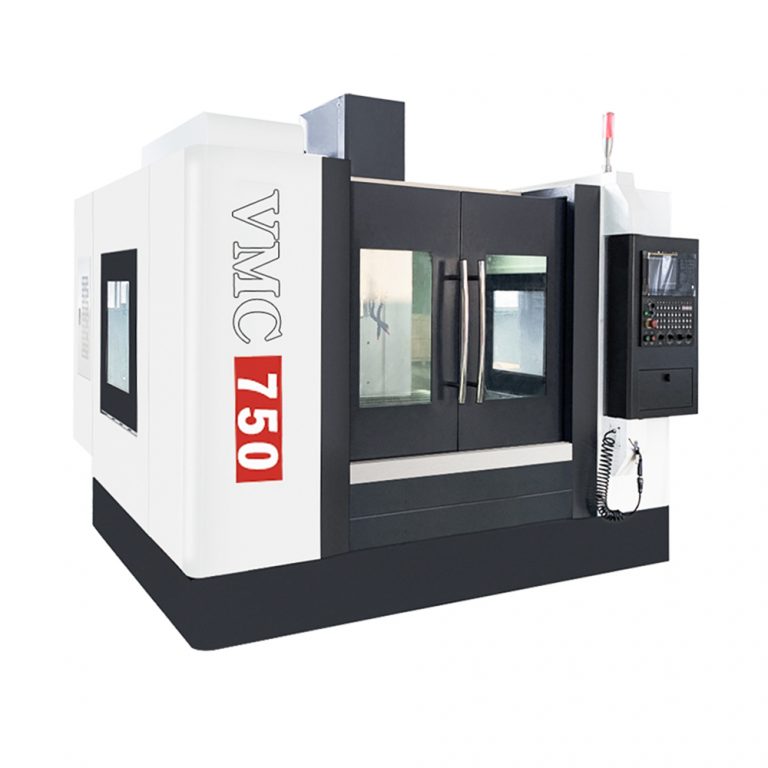
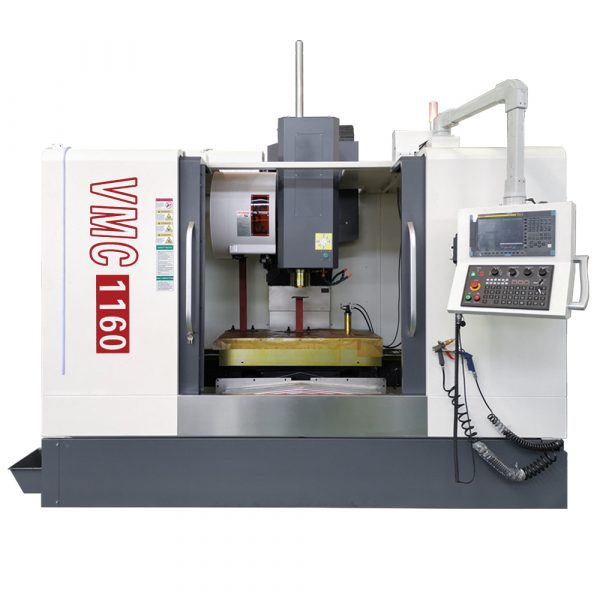
Now I want to shift forward. Imagine a shop that blends smart diagnostics with better hardware choices — that’s the future I back. A modern cnc vertical machining center should be part-machine, part-data node. Edge computing nodes on the floor gather vibration, spindle load, and cycle times; that data feeds simple dashboards for the team. With that, you can spot a failing bearing before it wreaks havoc. We’ve run pilot tests where predictive alerts trimmed unplanned downtime by nearly 25% — real numbers, seen on the logbook.
Real-world impact?
Yes. Shops that adopt these principles report cleaner shift handovers and steadier throughput. They standardise tool libraries, commit to routine spindle balancing, and keep CAM exports consistent. The comparison is stark: the old way reacts; the new way anticipates. This isn’t sci-fi. It’s about pairing robust mechanical design with smart monitoring. And if you’re wondering about costs — start small. Add sensors to your high-use machines first. Scale out as confidence grows. — the results compound.
To wrap this up, here are three practical evaluation metrics I always share when teams ask how to choose upgrades or suppliers:
1) Mean Time Between Failures (MTBF) improvement potential — look for measurable uplift, not vendor promises. 2) Integration readiness — can the machine export logs, link to your ERP or CAM, and accept simple diagnostics? 3) Total cost of ownership over five years — include consumables, service intervals, and expected productivity gains. Use those three as your checklist. I stand by them; they’ve guided my buying calls and my shop-floor fixes.
In the end, I’m pragmatic. Machines need to work, people need to feel supported, and managers need results. If you want a partner that knows both the hardware and the human side of the shop, take a look at Leichman. We’ve seen the problems, fixed many of them, and learned to respect the people who run the floor.