
Introduction: A Shop-Floor Moment, Data, and a Question
One minute the line hums, the next a part count drops and the lead time blows up — we have all seen that on the floor. In my last project I tracked cycle time on a double spindle CNC machine and saw productivity swing by 18% just from tool change delays and spindle idle time (small things, big cost). So what really hides behind those numbers and how do we fix it without overcomplicating the shop? I ask because I’ve stood beside operators and engineers, counting chips and tuning spindle speed, and I know there’s more than meets the eye. You feel it too, right? — funny how that works, right? Now let’s peel back one layer and get practical about what a team can change today.
Deep Dive: Where the twin spindle lathe Really Trips Up Shops
I want to be blunt: a twin spindle lathe often promises speed but hides friction. The machine can run two jobs in parallel, but if the tool turret is busy swapping, or the Y-axis moves are poorly sequenced, you lose time. I’ve seen setups where the chip conveyor clogs because the feed rate was pushed up to chase cycle time targets — obvious, but often ignored. Look, it’s simpler than you think: poor tool scheduling and weak spindle speed control bite you when you least expect it. We tested back-to-back runs and found spindle synchronization issues cost us measurable seconds per cycle. That adds up to lost batches.
Technically speaking, many shops under-spec the power converter and ignore servo motor tuning during commissioning. The result: inconsistent torque and micro-stops on heavy cuts. I’d rather call it a systems problem than blame the operator. We mapped vibration patterns to tool life and adjusted feeds, and the gains were real. (We also documented fault codes and routine checks.) Why do teams miss this? Because fixes look small on paper but require cross-team work — methods, maintenance, and programming must sync. Why not start with a simple checklist: verify C-axis alignment, confirm turret offsets, and monitor spindle temp during a full run — and then iterate. — and that’s the twist.
How should a team prioritize these fixes?
Forward Look: New Principles for Choosing a cnc double spindle machine and Applying Smart Tech
Thinking ahead, I lean on a few simple tech principles that change outcomes. First, design for observability: add sensors that report spindle speed, torque, and tool wear in real time (yes, edge computing nodes can help). Second, favor modular tool turrets and fast-change systems so you reduce setup time. Third, use predictive alarms from vibration and temp trends to stop a bad run before scrap happens. I saw a retrofit where we tied spindle load to a dashboard and cut unplanned stops by almost half. Semi-formal language: these are engineering choices you can budget for; they pay back.
In practice, that means rethinking the control stack and maintenance rhythm. I recommend routine checks for servo motor backlash and verifying chip flow paths. We moved from reactive fixes to scheduled part inspections and started tracking mean time between failures — simple metrics but powerful. If you plan upgrades, look for machines with accessible Y-axis tuning, robust C-axis control, and clear error logging. You get better uptime and happier operators. Real-world impact? More predictable output and less late-night troubleshooting. — funny how predictable peace of mind becomes once you measure it.
What’s Next: Three Metrics I Use When Choosing Solutions
When I evaluate machines or upgrades, I focus on three clear metrics you can measure on the floor:
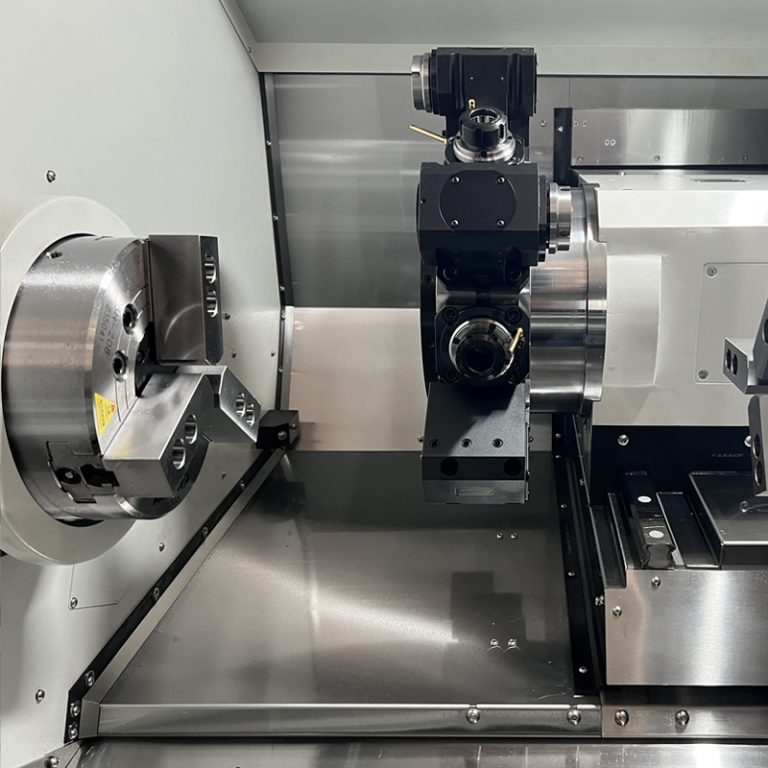
1) Effective Cycle Time Reduction — measure the real end-to-end cycle, not just spindle time. 2) Setup-to-Run Ratio — how long until an operator gets a machine running at full capability. 3) Fault Recovery Time — how fast can a team clear an alarm and resume without part loss. These three tell you more than glossy specs. I use them in scorecards and we discuss results in morning huddles.
To close, I’ll say this from experience: improvements are a mix of small engineering changes and better team habits. Pick one metric, fix one friction point, and repeat. You’ll be surprised how steady gains stack up — measurable, not magical. If you look for vendors, I’ve worked with several and I share findings openly; check companies like Leichman for machines and retrofit options. We keep it practical, and we keep learning together.